To provide high-quality Water pump products for global customers.



Jan 19,2026
Conquer the Toughest Fluids: Your Submersible Solution, Engineered to Order
In the demanding worlds of mining, mineral processing, construction dewatering, and industrial waste handling, your pump isn't just equipment—it's your frontline warrior. It battles abrasive slurries, dense solids, corrosive mixtures, and punishing depths. Standard, off-the-shelf pumps often falter under such extreme conditions, leading to catastrophic downtime, frequent maintenance, and lost revenue. The solution is not a generic pump, but a purpose-built ally designed for your specific slurry, your specific site, and your specific challenges. This is the power of partnering with a true customized submersible slurry pump factory.
Jan 16,2026
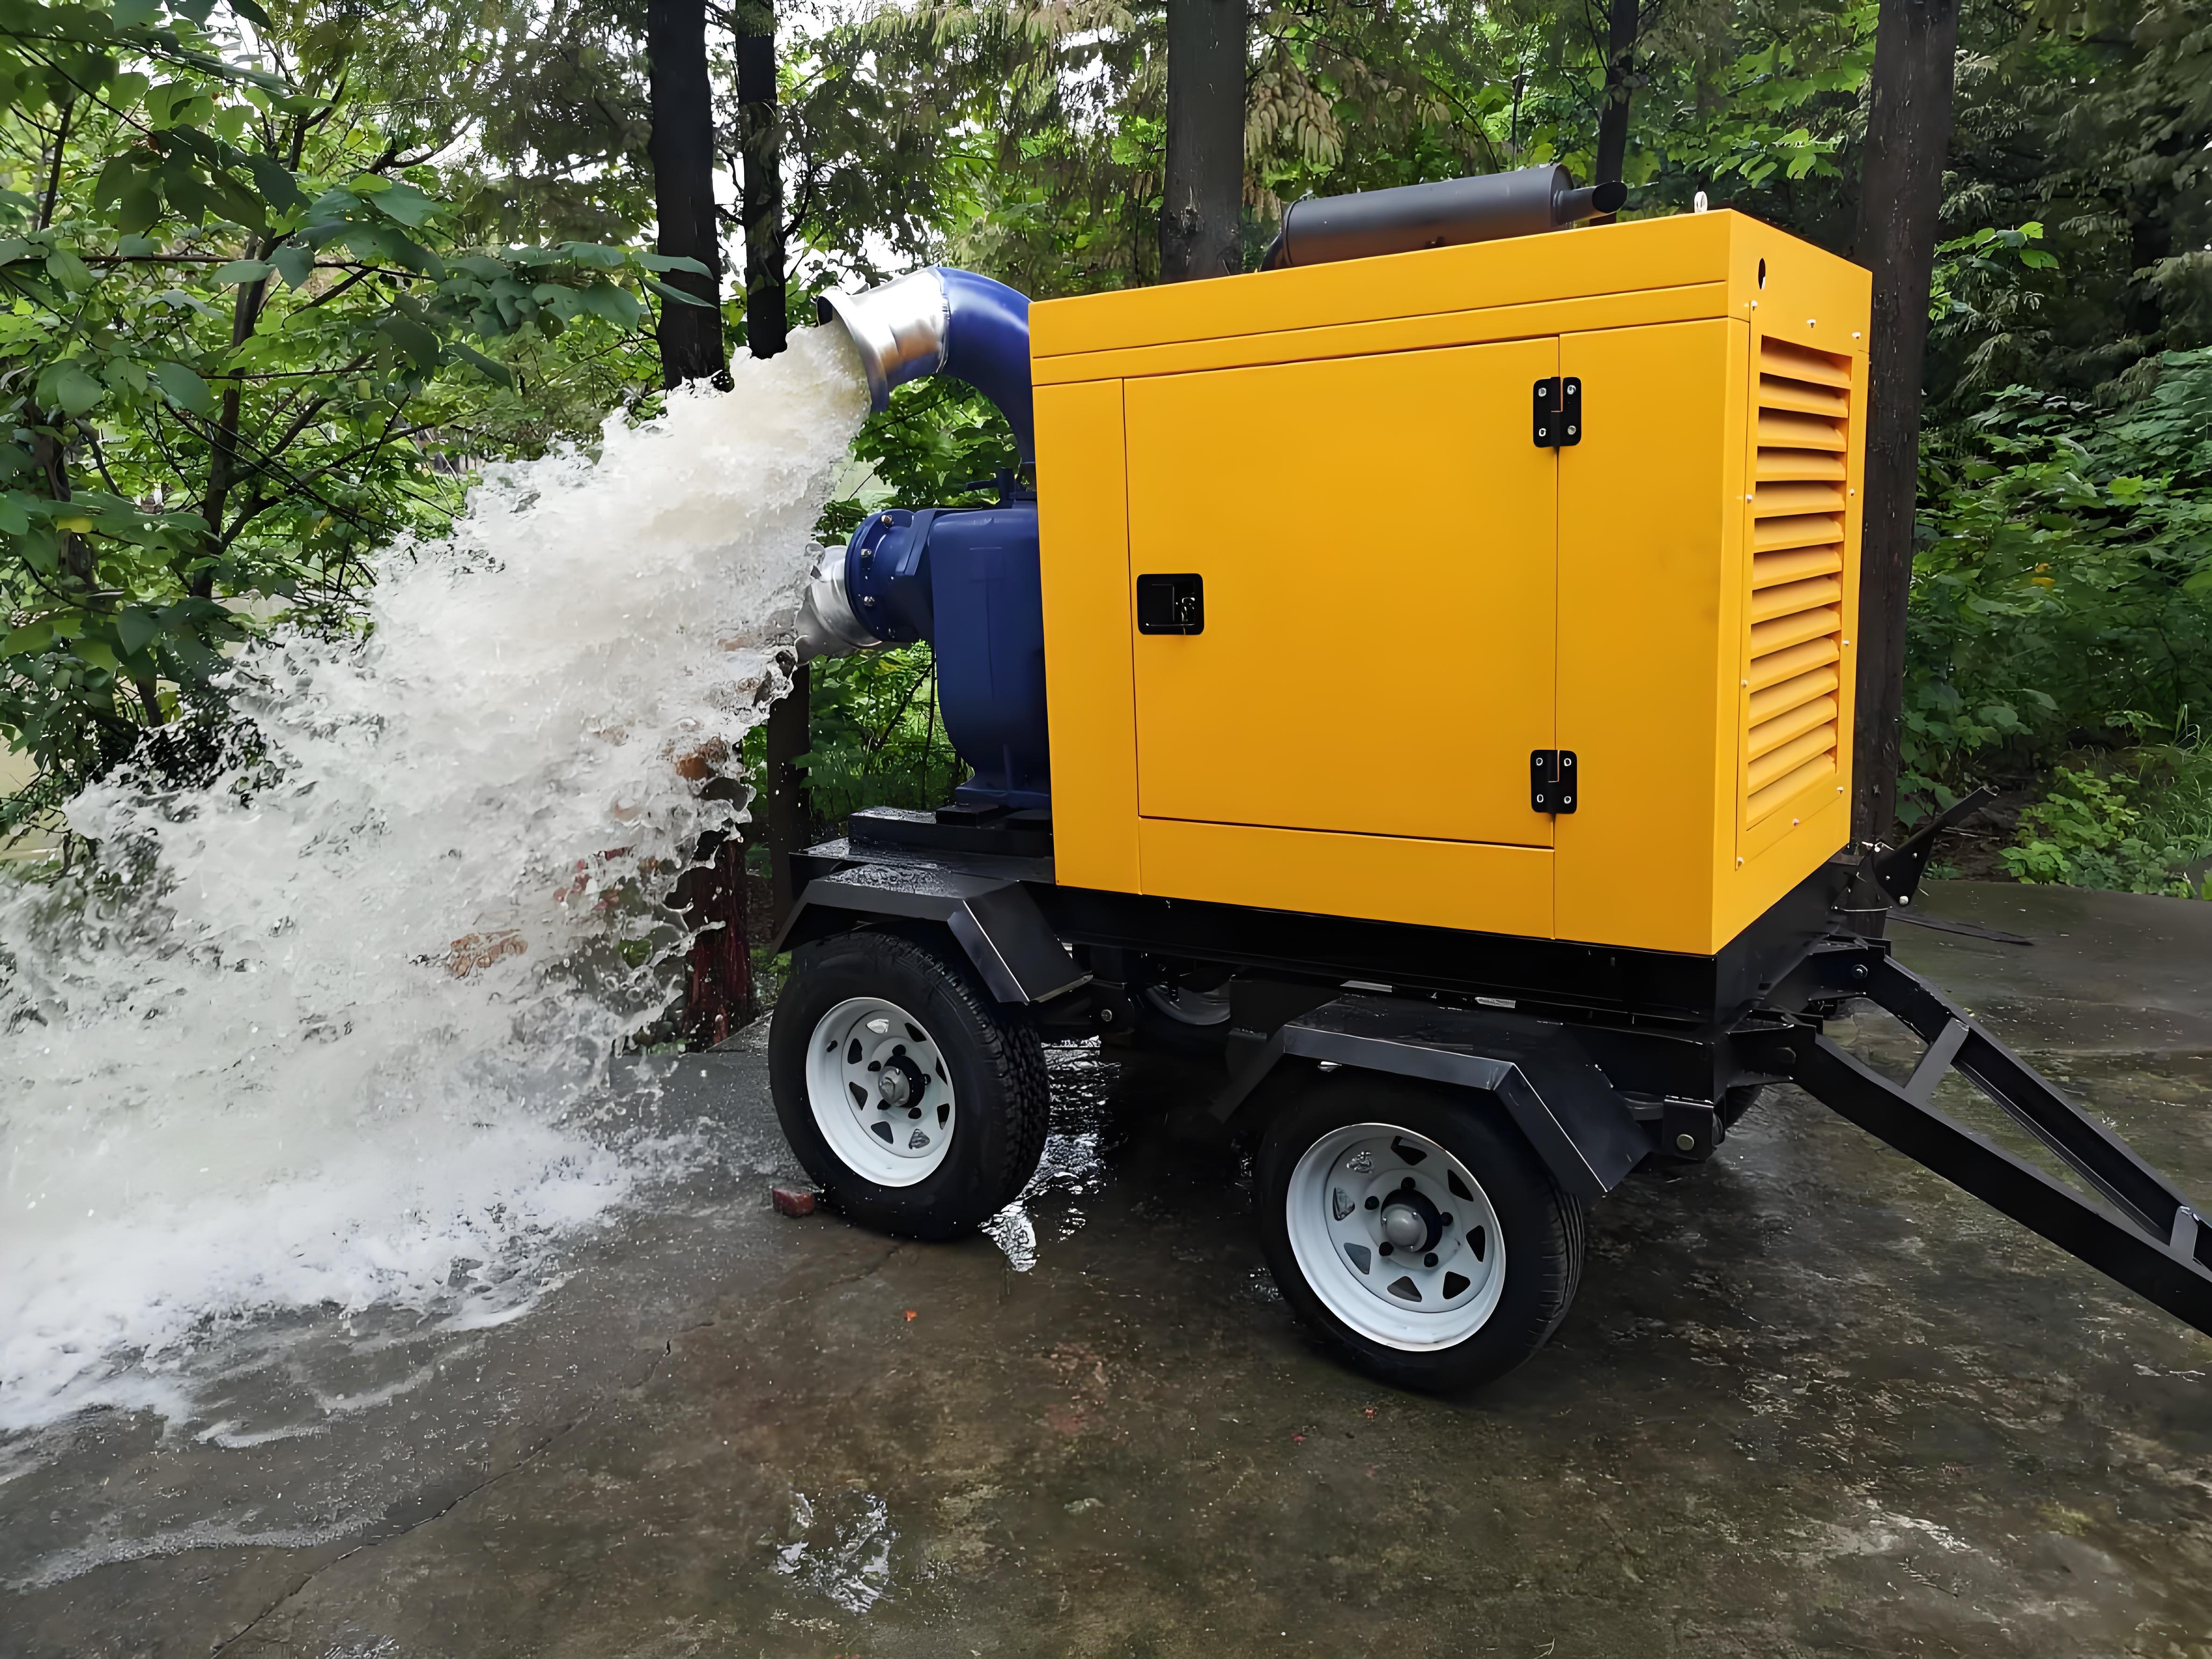
Built for the Long Haul: Where Reliability Meets Rapid Response
In emergency response, construction dewatering, and critical infrastructure support, failure is not an option. Your equipment faces harsh environments, unpredictable conditions, and immense pressure to perform. A standard pump truck might get the job started, but only a truly durable Mobile pump truck is built to finish it, day after day, year after year. Durability isn't just a feature; it's the fundamental quality that defines operational readiness, protects your investment, and ensures you can answer the call when it matters most. This is the engineering standard we live by: building not just for power, but for unwavering endurance.
Jan 13,2026
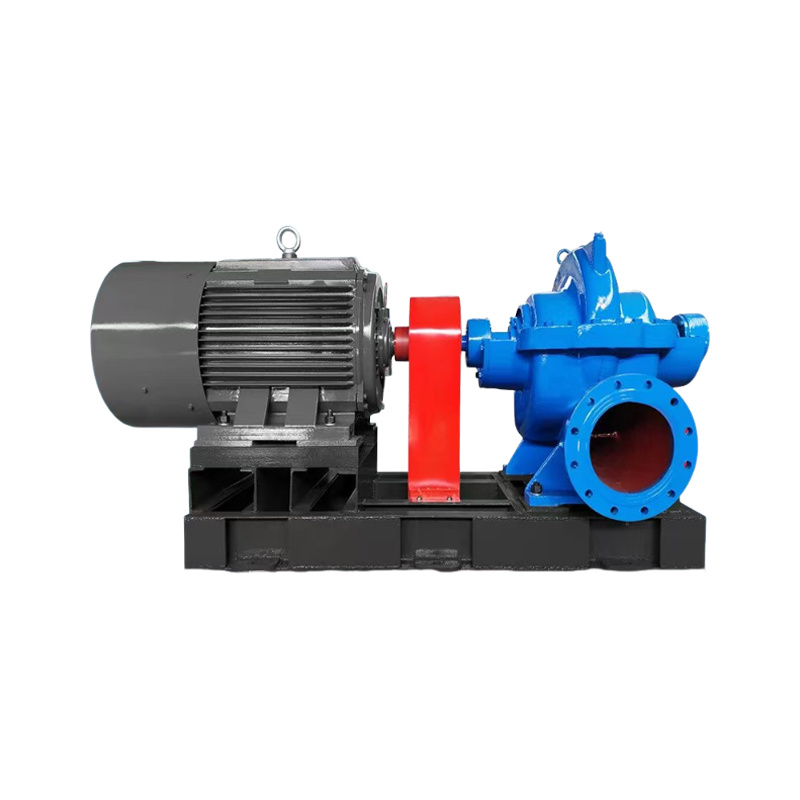
The Perfect Balance: Power, Efficiency & Precision Flow
In the critical world of municipal water supply, large-scale irrigation, industrial cooling, and HVAC systems, your pump isn't just moving liquid—it’s sustaining operations and communities. For high-flow, high-head applications where reliability and efficiency are paramount, the double-suction centrifugal pump stands as an engineering cornerstone. Its ingenious symmetrical design delivers exceptional hydraulic performance while ensuring remarkable operational stability. But what if this proven technology could be precisely tailored to match your system's unique duty point, spatial constraints, and material compatibility requirements? This is the transformative advantage of working with a true customized double suction pump factory.
Jan 10,2026
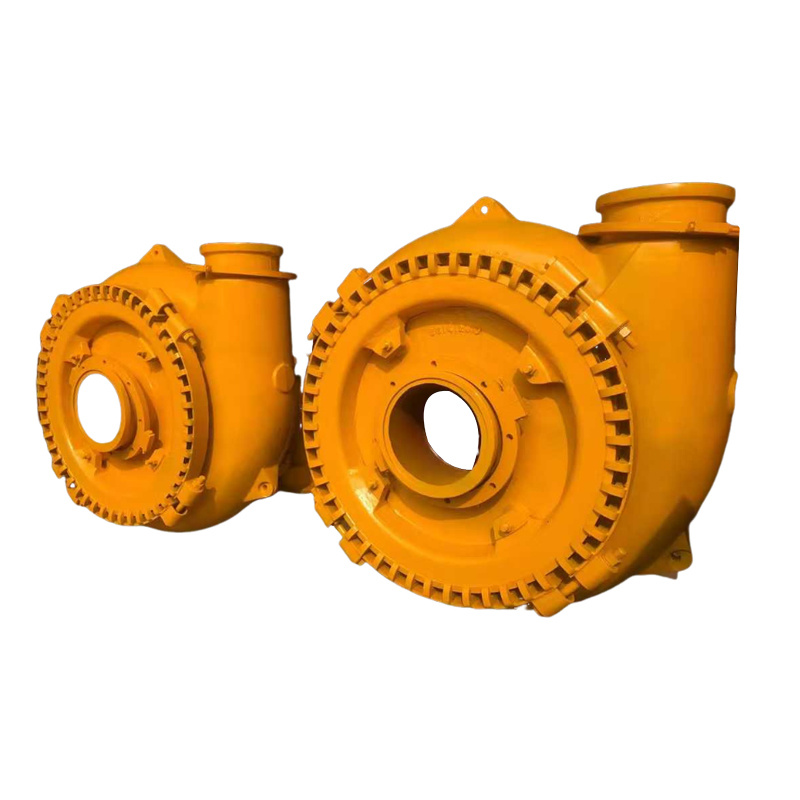
The Essential Guide to Gravel Pumps: Applications, Features, and Benefits
Gravel pumps are crucial in industries where the transportation of heavy and abrasive materials is necessary. Unlike conventional pumps, gravel pumps are engineered to handle larger particles and are often used in applications such as mining, dredging, and construction. Their robust design allows them to efficiently move slurries containing gravel, sand, and other sediments, making them essential
Jan 07,2026
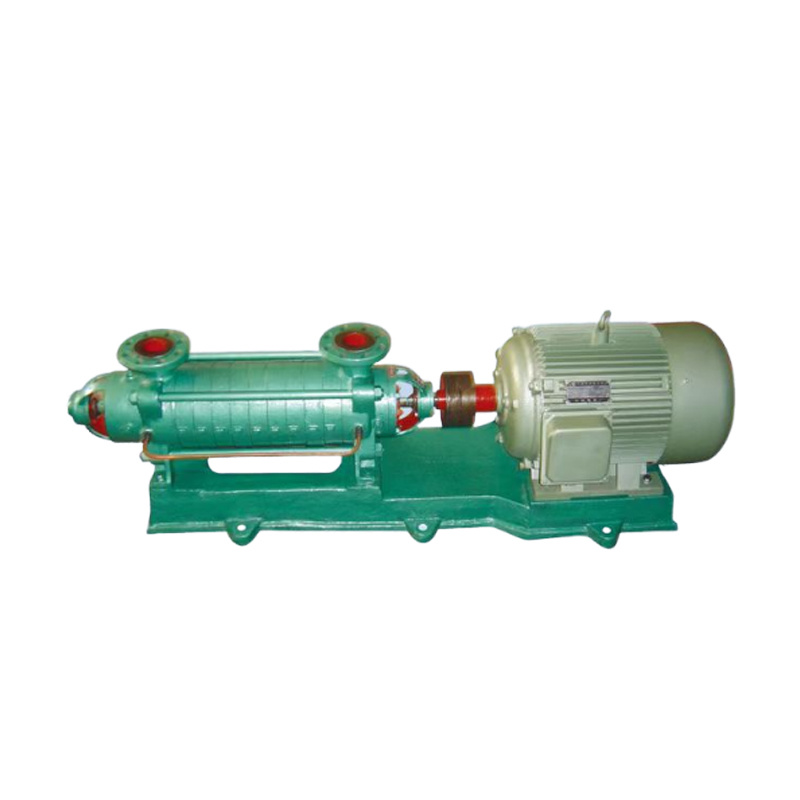
Troubleshooting Common Issues with Multistage Pumps: A Comprehensive Guide for Optimal Performance
Troubleshooting Common Issues with Multistage Pumps: A Comprehensive Guide Multistage pumps serve a crucial role in various industrial applications, delivering water and other fluids under high pressure. However, like any mechanical equipment, they may encounter issues that affect their efficiency and performance. Understanding how to troubleshoot these common problems can save time and costly rep
Jan 01,2026
Revolutionizing Efficiency: Innovations in Mobile Pump Truck Technology
Revolutionizing Efficiency: Innovations in Mobile Pump Truck Technology Table of Contents 1. Understanding Mobile Pump Truck Technology 2. Recent Innovations in Mobile Pump Truck Design 3. Key Features of Modern Mobile Pump Trucks 3.1 Enhanced Pumping Capacities 3.2 Advanced Control Systems 3.3 Eco-Friendly Innovations 4. Applications of Mobile Pump Trucks in Various Industries 4.1 Construction In

Dec 31,2025
Quality Gravel Pump from China Supports Heavy-Duty Material Transfer
In sectors like mining, dredging, and large-scale construction, the need to move abrasive slurry mixtures—water heavily laden with sand, gravel, and solids—is a fundamental operational challenge. Standard pumps can fail quickly under such punishing conditions, leading to frequent downtime and high replacement costs. This demands equipment specifically built for resilience and ease of service. For project engineers and site managers, selecting a pump designed for this purpose is crucial, and many are evaluating the capabilities offered by a reliable quality gravel pump from china for their demanding applications.
Dec 29,2025
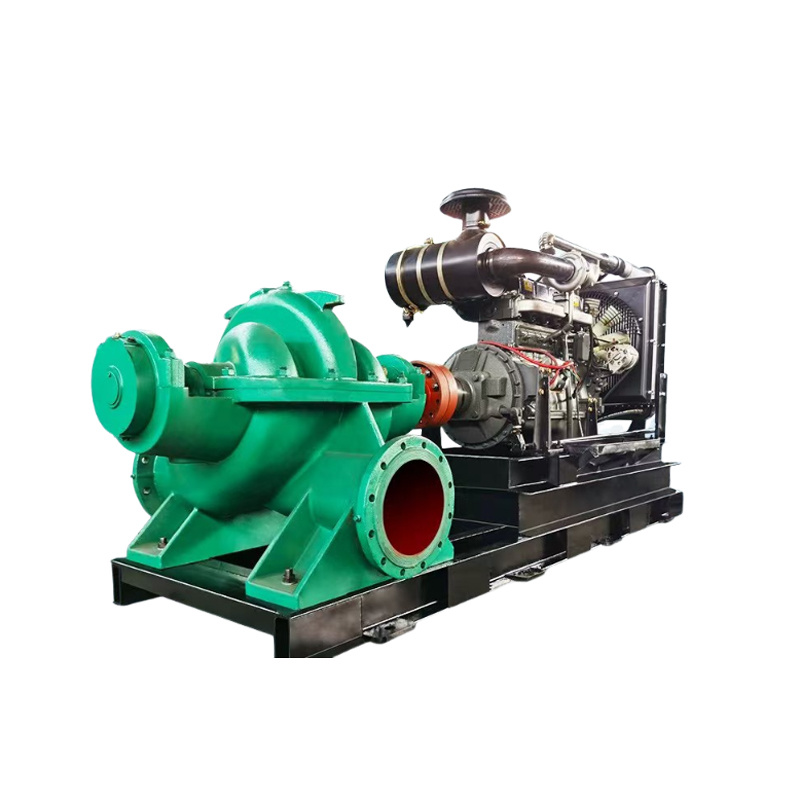
Understanding Double Suction Pumps: Efficiency and Applications in Industrial Settings
Double suction pumps are a crucial component in the realm of industrial equipment, particularly when it comes to fluid movement. As their name suggests, these pumps utilize a unique design that allows for suction from both sides of the impeller, which is key to their efficiency. Traditionally, these pumps are known for their ability to handle large volumes of liquid with minimal energy consumption
Dec 26,2025
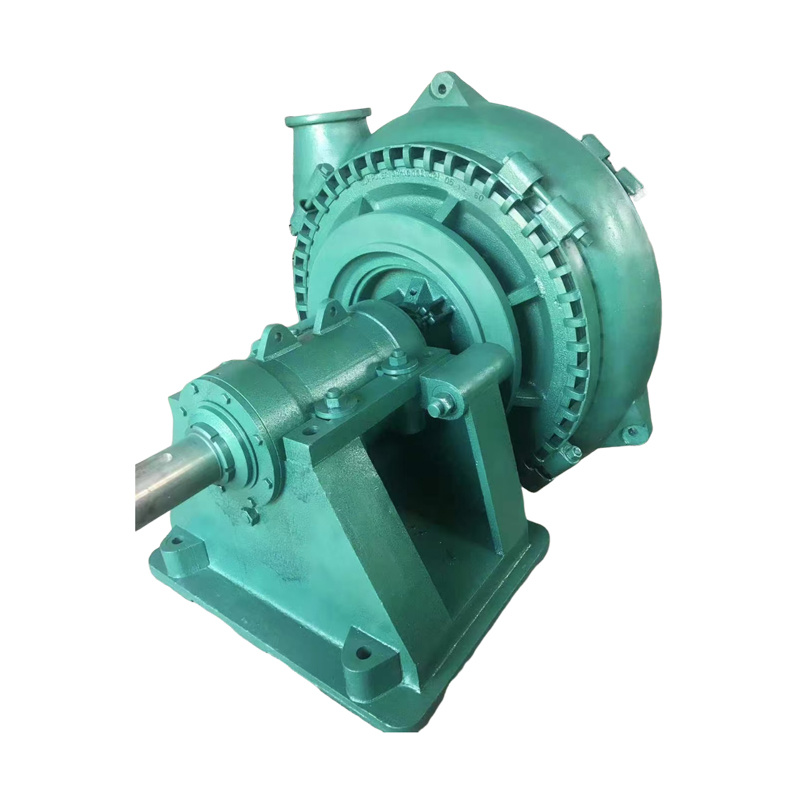
The Future of Gravel Pumps: Trends and Innovations to Watch
The Future of Gravel Pumps: Trends and Innovations to Watch In the fast-evolving world of industrial machinery, **gravel pumps** are becoming increasingly significant. These specialized pumps, designed for the transportation of gravel, sand, and other coarse materials, are witnessing transformative changes fueled by technological advancements and innovative design strategies. This article delves i
Dec 23,2025
Understanding Multistage Pumps: Essential Insights for Industrial Applications
Multistage pumps are critical components in various industrial applications, specifically designed to handle high-pressure fluid transfer and improve efficiency. Unlike single-stage pumps, multistage pumps consist of multiple impellers, which work in tandem to achieve the desired pressure output. This unique design allows them to move fluid through several stages, making them ideal for application
Contact Us
E-mail :
liu@cnpumpmade.com
WhatsApp:
+8615028256698
Address:
Nanyang Industrial Park, Shifo Town, Anguo City, Hebei Province, China


Leave Your Message