To provide high-quality Water pump products for global customers.

Understanding Submersible Slurry Pumps: Essential Insights for Industrial Applications
Nov 21,2026
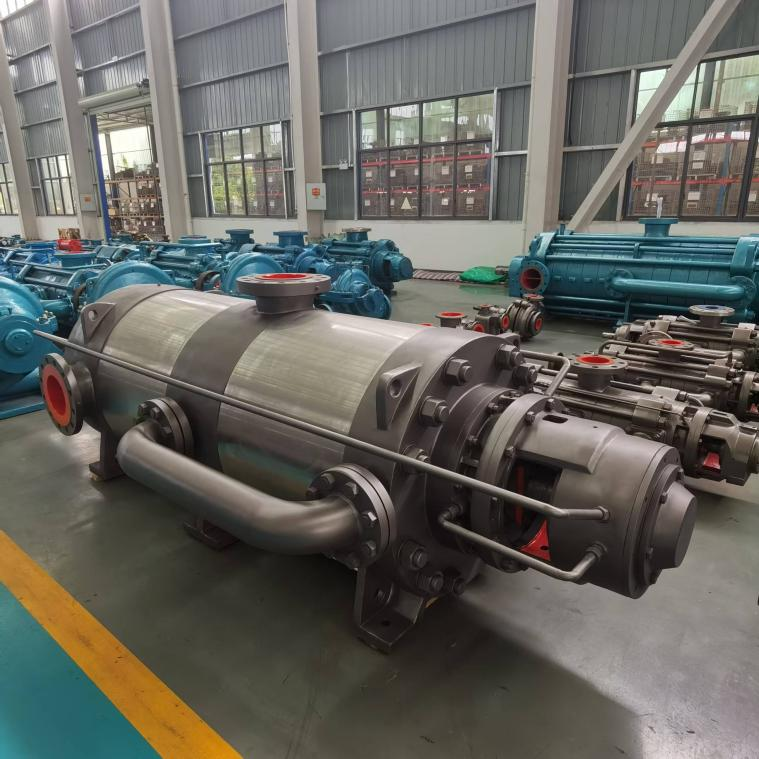
Submersible slurry pumps are specialized industrial pumps designed to efficiently transport abrasive and viscous fluids, often containing solid particles or slurries. These pumps are submerged in the fluid they are pumping, making them particularly effective in environments where traditional pumps may struggle. Understanding the mechanics and applications of submersible slurry pumps can significantly benefit industries such as mining, construction, and wastewater treatment.
One of the primary advantages of submersible slurry pumps is their ability to operate under challenging conditions. Being submerged means that these pumps are not susceptible to cavitation, which can occur when a pump is not adequately primed or when the intake pressure is too low. Additionally, submersible slurry pumps are often designed with robust materials that can withstand the wear and tear caused by abrasive particles within the slurry, extending their service life and reducing maintenance costs.
The design of submersible slurry pumps typically includes a hermetically sealed motor, which prevents the ingress of fluids and protects the motor from damage. This feature is crucial in environments where water or slurry could compromise the pump's functionality. Moreover, their compact design allows for easy installation in confined spaces, making them ideal for applications in mining pits or other challenging sites.
A critical consideration when selecting a submersible slurry pump is the type of slurry being pumped. The composition, viscosity, and particle size of the slurry will influence the pump's performance. It's essential to choose a pump that can handle the specific characteristics of the slurry to ensure optimal efficiency and minimize the risk of pump failure.
In terms of applications, submersible slurry pumps are widely used in various industries. In mining operations, they are used to remove excess water from pits and transport slurries for mineral processing. In construction, they are essential for dewatering excavations and managing site runoff. Additionally, in wastewater treatment facilities, submersible slurry pumps play a vital role in handling sludge and transporting it to treatment areas.
In conclusion, submersible slurry pumps are indispensable tools in many industrial settings due to their ability to handle abrasive, viscous fluids while maintaining high efficiency under challenging conditions. By understanding the principles behind these pumps, professionals can make informed decisions that enhance operational efficiency and reduce maintenance requirements in their respective fields. Embracing the advantages of submersible slurry pumps can lead to significant improvements in productivity and cost-effectiveness in industrial applications.
One of the primary advantages of submersible slurry pumps is their ability to operate under challenging conditions. Being submerged means that these pumps are not susceptible to cavitation, which can occur when a pump is not adequately primed or when the intake pressure is too low. Additionally, submersible slurry pumps are often designed with robust materials that can withstand the wear and tear caused by abrasive particles within the slurry, extending their service life and reducing maintenance costs.
The design of submersible slurry pumps typically includes a hermetically sealed motor, which prevents the ingress of fluids and protects the motor from damage. This feature is crucial in environments where water or slurry could compromise the pump's functionality. Moreover, their compact design allows for easy installation in confined spaces, making them ideal for applications in mining pits or other challenging sites.
A critical consideration when selecting a submersible slurry pump is the type of slurry being pumped. The composition, viscosity, and particle size of the slurry will influence the pump's performance. It's essential to choose a pump that can handle the specific characteristics of the slurry to ensure optimal efficiency and minimize the risk of pump failure.
In terms of applications, submersible slurry pumps are widely used in various industries. In mining operations, they are used to remove excess water from pits and transport slurries for mineral processing. In construction, they are essential for dewatering excavations and managing site runoff. Additionally, in wastewater treatment facilities, submersible slurry pumps play a vital role in handling sludge and transporting it to treatment areas.
In conclusion, submersible slurry pumps are indispensable tools in many industrial settings due to their ability to handle abrasive, viscous fluids while maintaining high efficiency under challenging conditions. By understanding the principles behind these pumps, professionals can make informed decisions that enhance operational efficiency and reduce maintenance requirements in their respective fields. Embracing the advantages of submersible slurry pumps can lead to significant improvements in productivity and cost-effectiveness in industrial applications.
PREVIOUS:
Contact Us
E-mail :
liu@cnpumpmade.com
WhatsApp:
+8615028256698
Address:
Nanyang Industrial Park, Shifo Town, Anguo City, Hebei Province, China


Leave Your Message