To provide high-quality Water pump products for global customers.


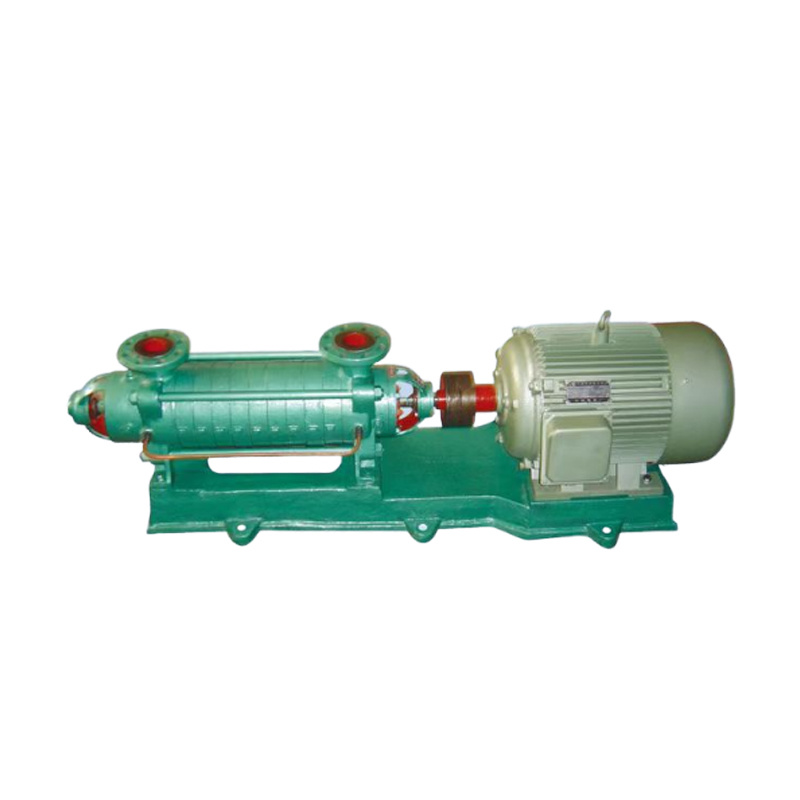
Understanding Multistage Pumps: Efficiency and Applications in Industrial Settings
Multistage pumps are essential components in various industrial applications, designed to transport fluids efficiently over significant distances and against high pressures. Unlike single-stage pumps, which utilize one impeller to generate pressure, multistage pumps incorporate multiple impellers (or stages) in series. This design enables them to achieve a higher pressure output, making them ideal
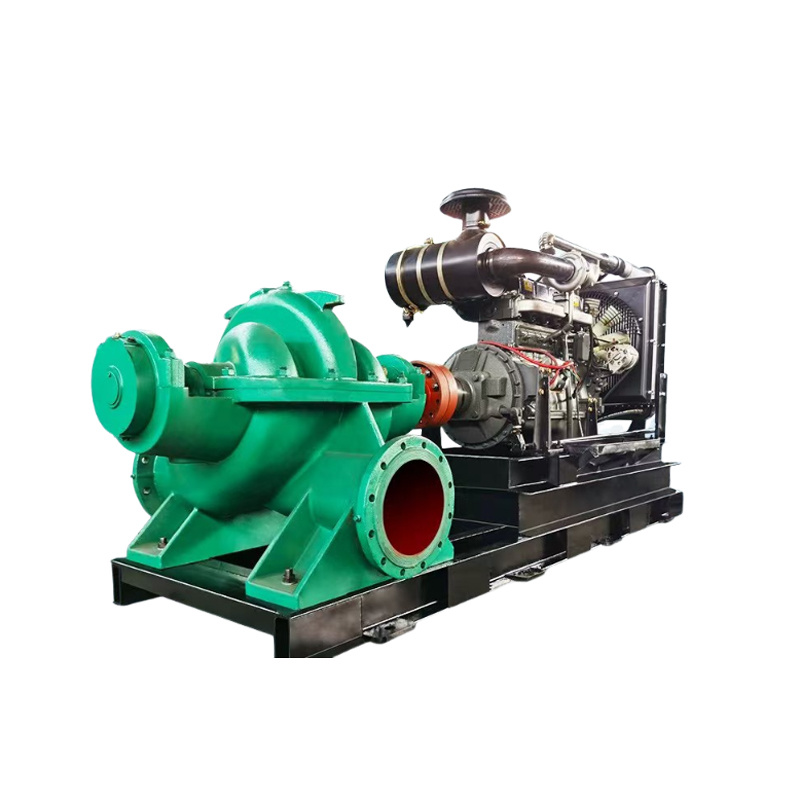
Understanding the Advantages and Applications of Double Suction Pumps
Double suction pumps, as the name suggests, are designed with two inlets that allow fluid to enter the impeller from both sides. This innovative design results in a balanced impeller, which minimizes vibration and extends the pump's operational life. One of the primary advantages of double suction pumps is their high efficiency. Since they handle larger volumes of fluids with lower energy consumpt

How to Properly Store and Preserve Your Gravel Pump During Off-Season
How to Properly Store and Preserve Your Gravel Pump During Off-Season
Storing and preserving your gravel pump during the off-season is crucial for maintaining its functionality and extending its lifespan. Proper storage techniques not only prevent damage but also ensure that the pump is ready for immediate use when the season starts again. In this comprehensive guide, we will cover everything you
Comprehensive Guide to Training Staff on Best Practices for Submersible Slurry Pump Operation
Training Staff on Best Practices for Submersible Slurry Pump Operation
Introduction to Submersible Slurry Pumps
Submersible slurry pumps are essential in various industries, including mining, construction, and wastewater management. These pumps are designed to handle abrasive and high-density materials, making them ideal for transferring slurries. Proper training for staff operating these pumps is
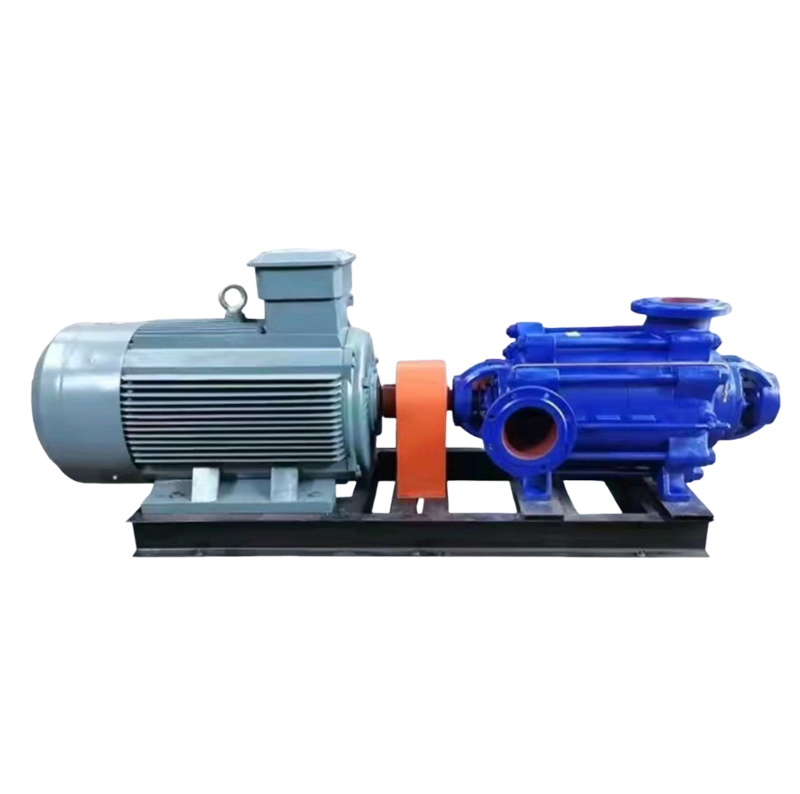
Double Suction Pumps: A Cost-Effective Solution for High-Volume Needs
Double Suction Pumps: A Cost-Effective Solution for High-Volume Needs
In the world of industrial pumps, efficiency and reliability are paramount, especially when dealing with high-volume applications. Among the various types of pumps available, **double suction pumps** stand out as a cost-effective solution designed specifically for **high-volume** requirements. This article delves deep into the m
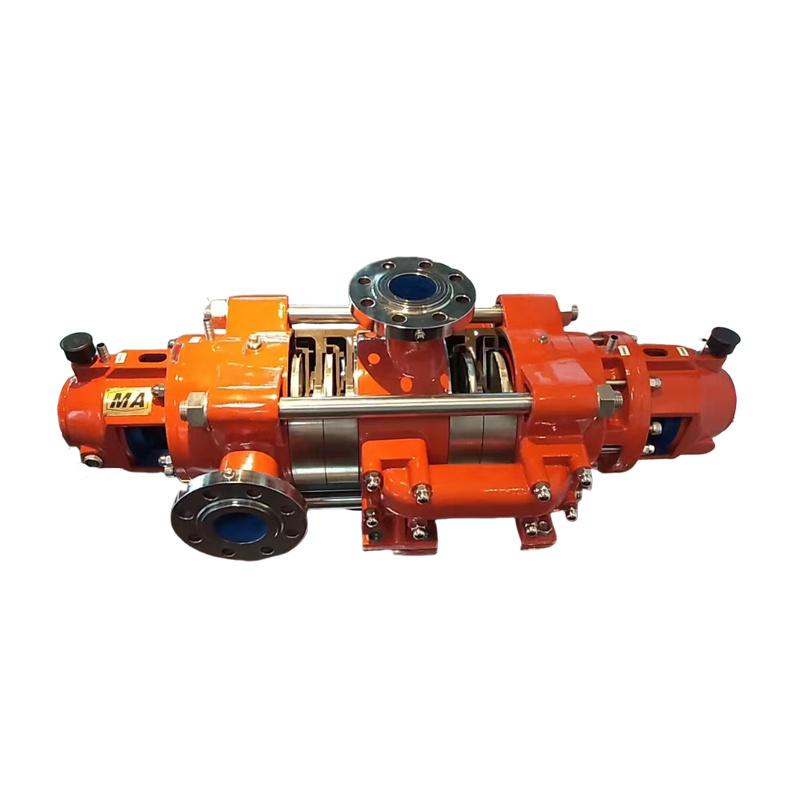
Multistage Pumps in Chemical Processing: Ensuring Safety and Efficiency
Multistage Pumps in Chemical Processing: Ensuring Safety and Efficiency
Table of Contents
1. Introduction to Multistage Pumps
2. Importance of Multistage Pumps in Chemical Processing
3. How Multistage Pumps Work
4. Key Applications of Multistage Pumps
4.1. Water Treatment
4.2. Chemical Circulation
4.3. Fuel and Oil Processing
5. Safety Considerations in Using Multistage Pumps
5


Leave Your Message