To provide high-quality Water pump products for global customers.



The Critical Role of Quality Assurance in Submersible Slurry Pump Manufacturing
The Critical Role of Quality Assurance in Submersible Slurry Pump Manufacturing
Table of Contents
Understanding Submersible Slurry Pumps
The Importance of Quality Assurance in Manufacturing
Key Quality Assurance Processes in Pump Manufacturing
Quality Control of Materials and Components
Comprehensive Testing Procedures for Slurry Pumps
Adhering to Industry Standards and Regulations
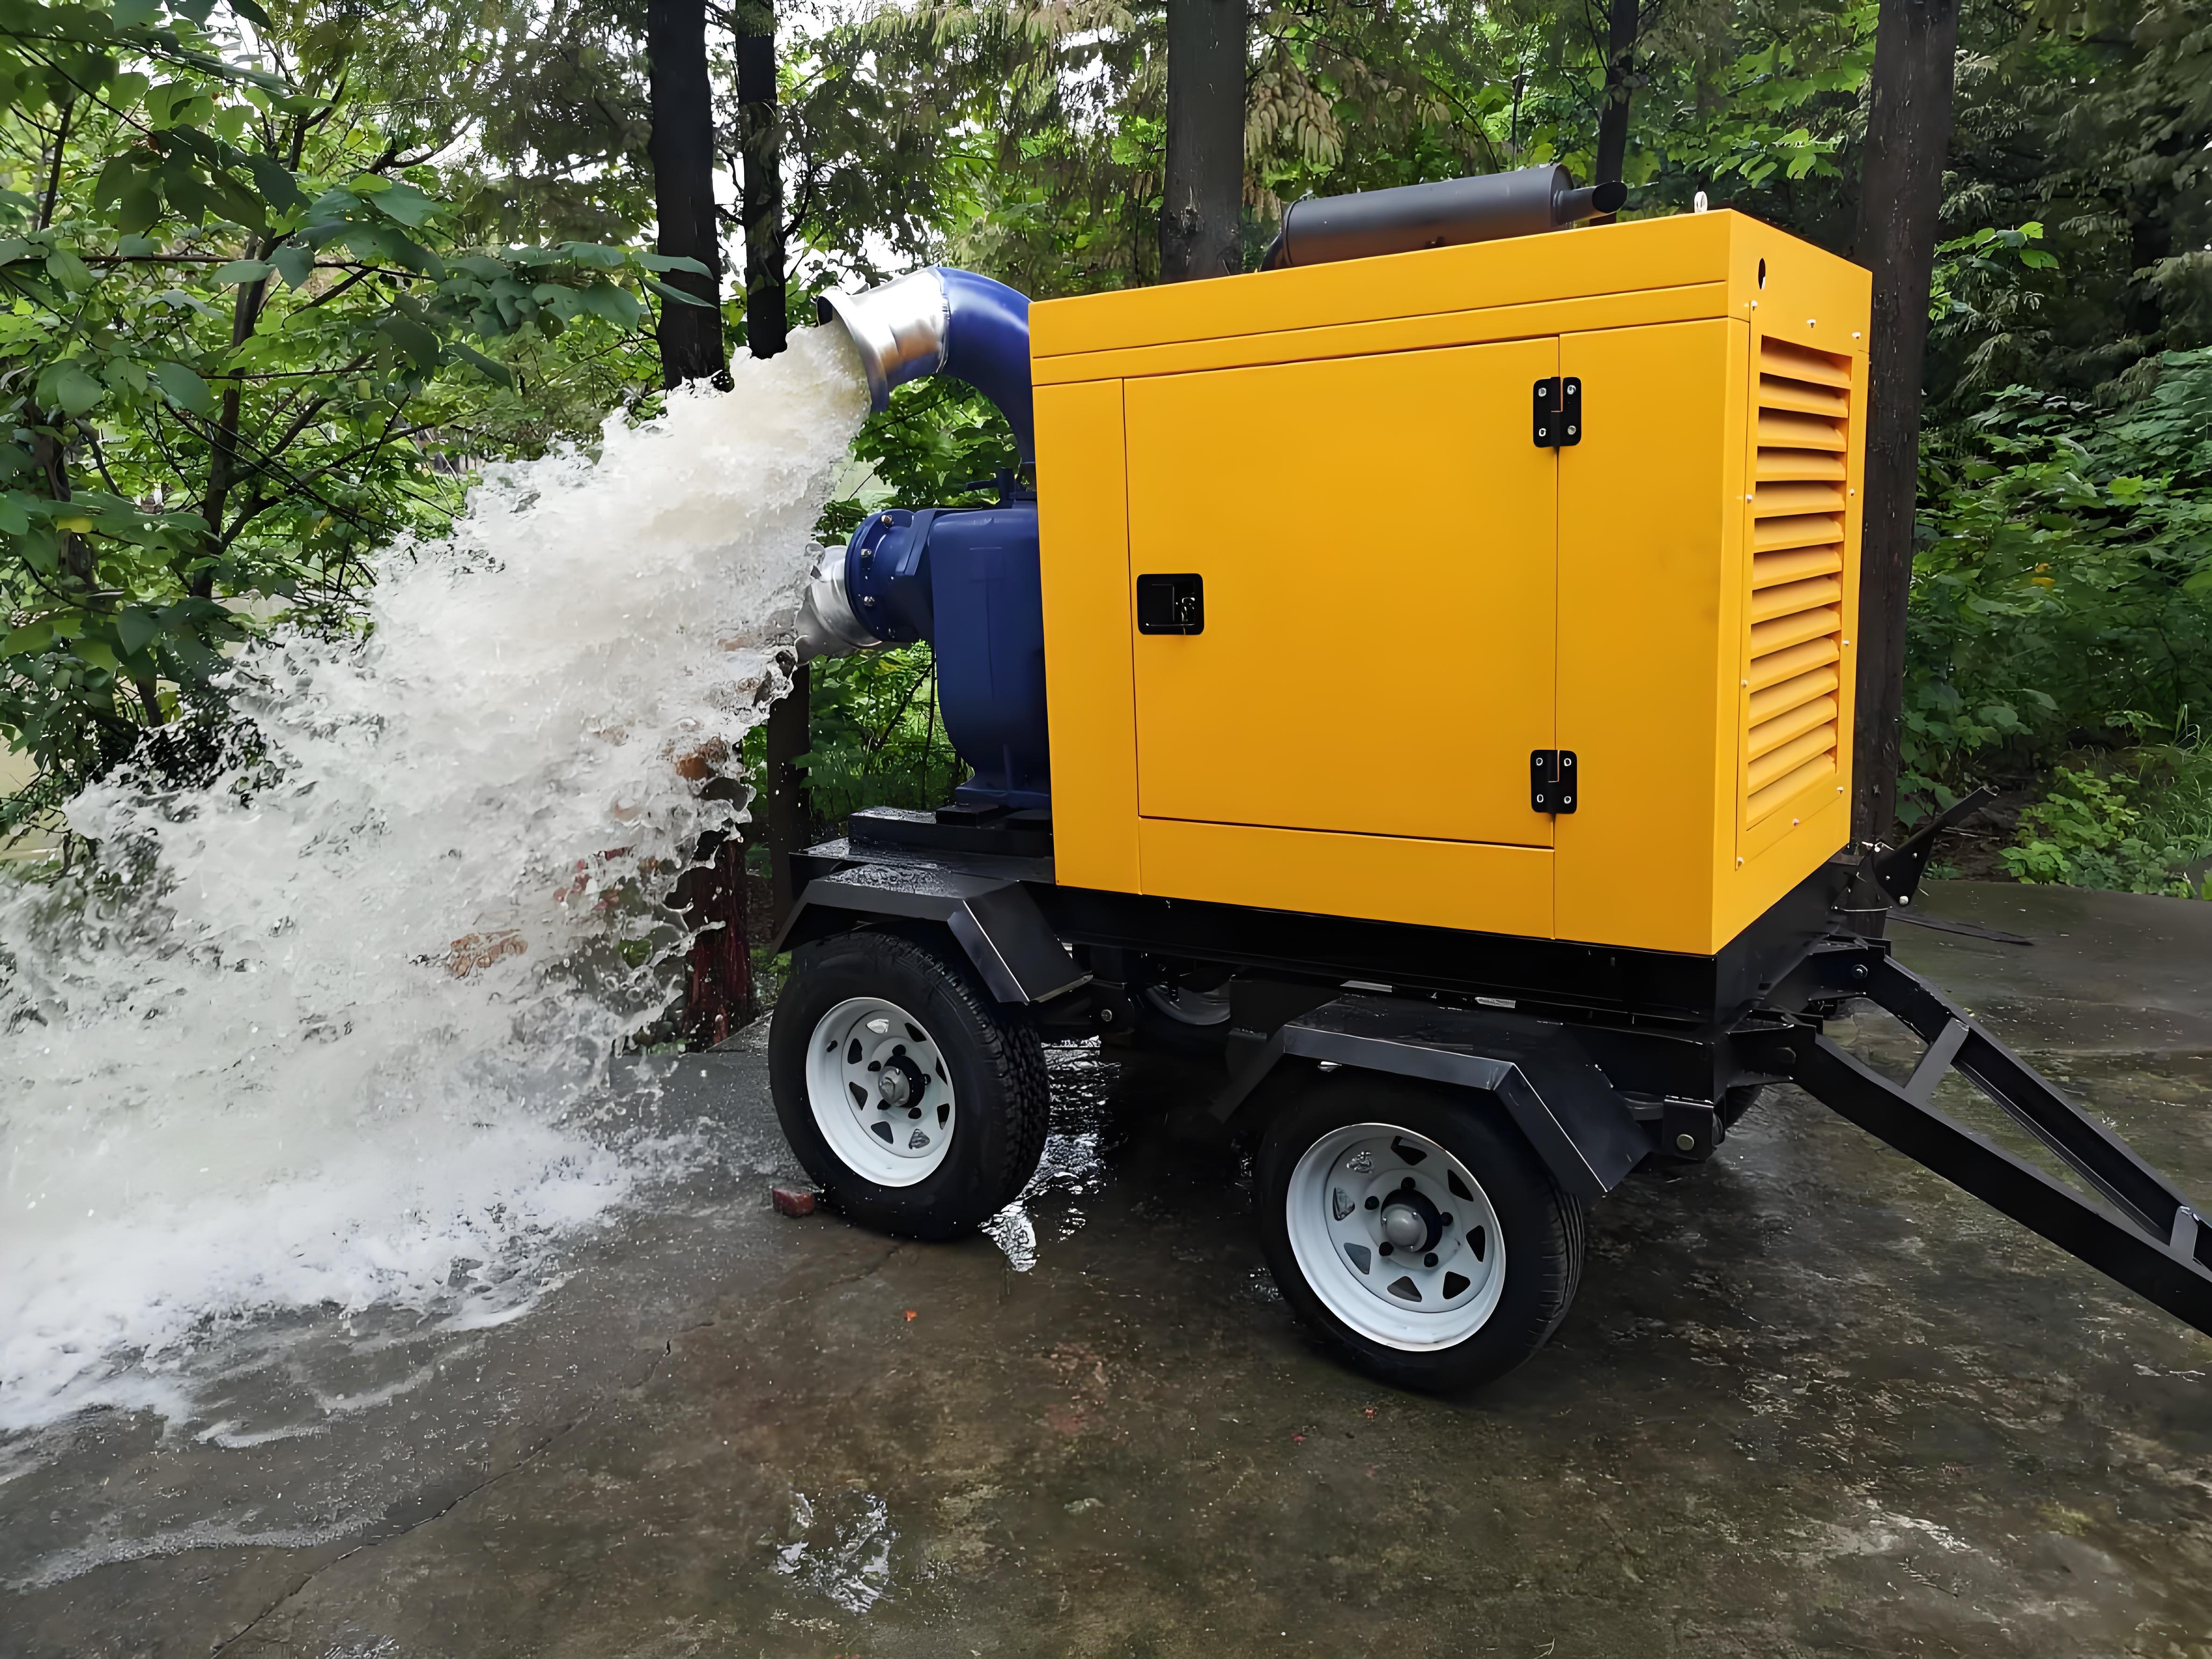
Understanding the Benefits and Applications of Mobile Pump Trucks
Mobile pump trucks are specialized vehicles designed to transport and operate pumping equipment at various job sites. Their primary function is to provide efficient fluid transfer solutions, making them essential in numerous industries, including construction, agriculture, oil and gas, and wastewater management.
One of the key benefits of mobile pump trucks is their mobility. Unlike stationary pum
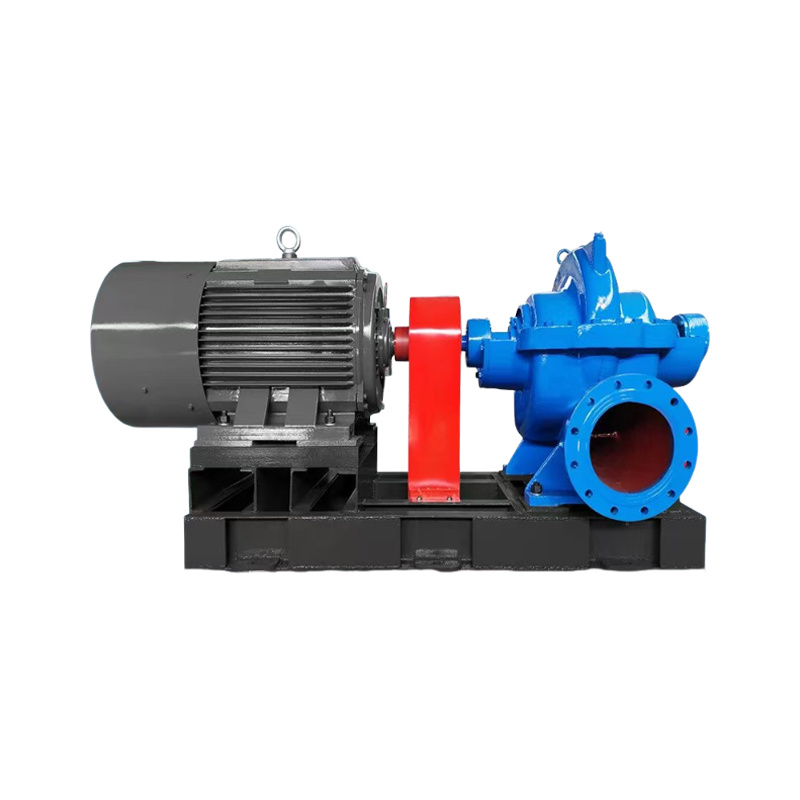
Sealing the Deal: How Double Suction Pumps Improve Efficiency
Sealing the Deal: How Double Suction Pumps Improve Efficiency
Table of Contents
1. Understanding Double Suction Pumps
2. The Design and Functionality of Double Suction Pumps
3. Advantages of Utilizing Double Suction Pumps
3.1 Increased Efficiency in Fluid Transport
3.2 Enhanced Performance and Reliability
4. Applications of Double Suction Pumps in Various Industries
4.1 Water and Wastewater Manage

Understanding Gravel Pumps: Essential Insights for Industrial Applications
Gravel pumps are specialized industrial pumps designed primarily for transporting abrasive and heavy solid materials, particularly gravel, sand, and other similar substances. They play a crucial role in various industries, including mining, construction, and dredging, where the efficient movement of these materials is essential for productivity and operational effectiveness. Understanding the func
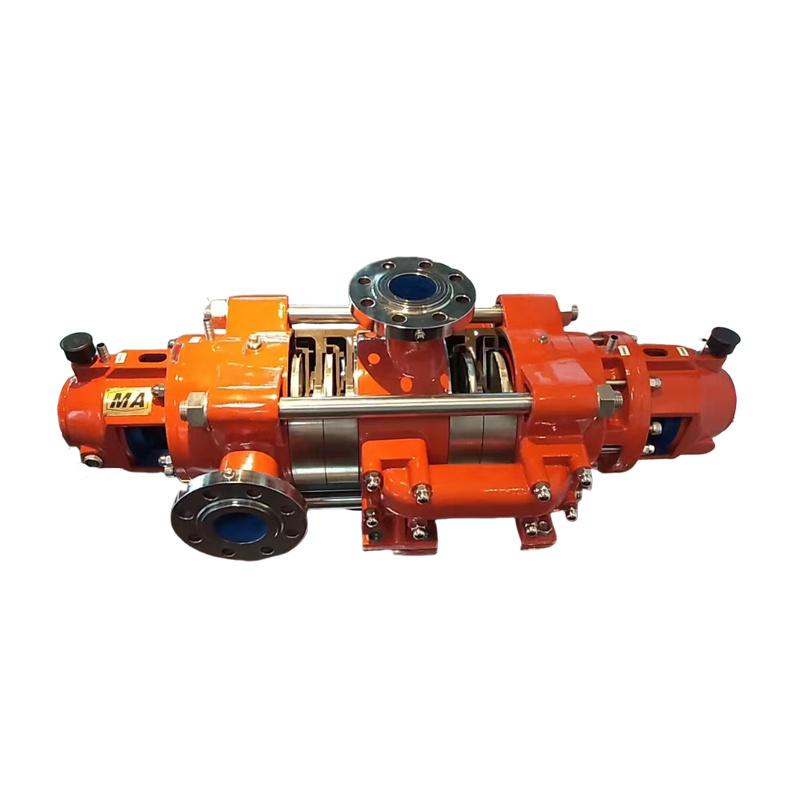
Real-World Case Studies: Success Stories with Multistage Pumps
Real-World Case Studies: Success Stories with Multistage Pumps
Table of Contents
Introduction to Multistage Pumps
Benefits of Multistage Pumps in Industrial Applications
Case Study 1: Water Supply Solutions for Municipalities
Case Study 2: Enhanced Oil Recovery in the Petrochemical Industry
Case Study 3: Precision Agriculture and Irrigation
Case Study 4: HVAC Systems in Co
Essential Insights on Submersible Slurry Pumps for Industrial Applications
Submersible slurry pumps are integral to various industrial processes, particularly in sectors such as mining, construction, and wastewater management. These pumps are specifically designed to handle abrasive and viscous materials, making them ideal for transporting slurry—mixtures of solids and liquids.
**Design and Functionality**
The primary feature of a submersible slurry pump is its ability t


Leave Your Message