To provide high-quality Water pump products for global customers.


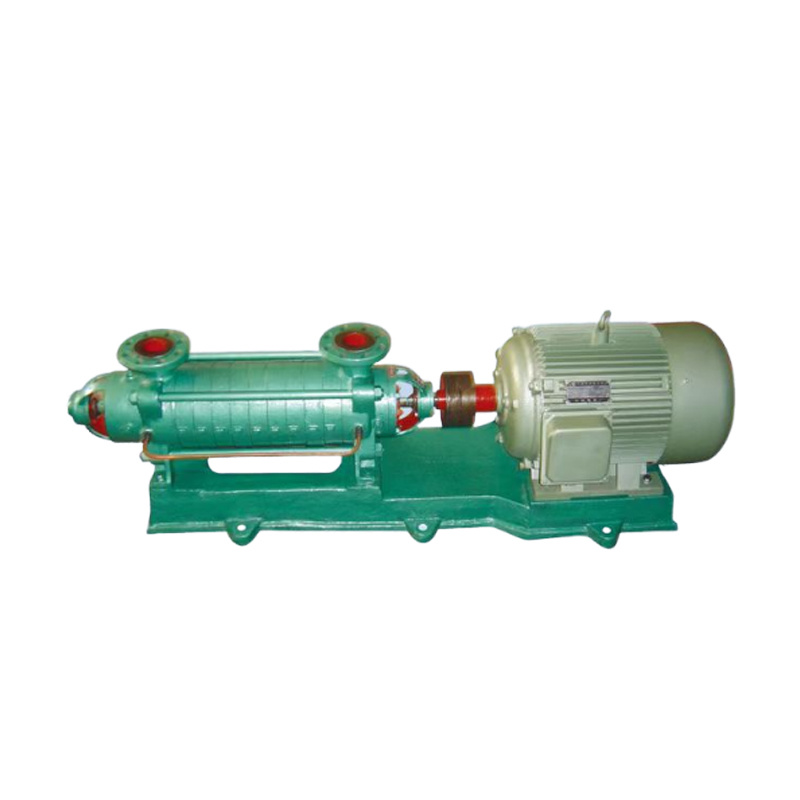
Customize Multistage Pump Technology Meets Diverse High-Pressure Application Needs
Industrial operations requiring efficient high-pressure liquid transfer are increasingly turning to customize multistage pump solutions to meet their specific operational demands. Manufacturers specializing in these systems, particularly those based in China, are offering tailored designs that provide optimal performance across various industries including water treatment, boiler feed systems, and industrial cleaning applications. The ability to customize multistage pump configurations allows users to achieve precise pressure and flow characteristics while maintaining energy efficiency.

Understanding Submersible Slurry Pumps: Key Features and Applications
Submersible slurry pumps are vital components in industries where the transportation of abrasive liquids and slurries is necessary. These pumps are specifically designed to operate underwater, making them ideal for applications in mining, construction, and wastewater treatment. The unique construction of a submersible slurry pump allows it to handle tough materials that traditional pumps may not m
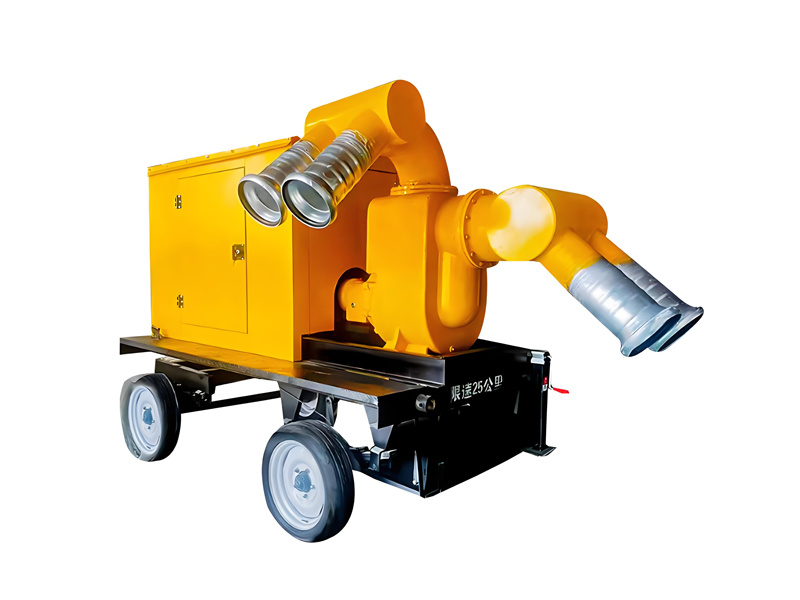
Newest Mobile Pump Truck Models Enhance On-Site Fluid Handling Capabilities
The fluid handling industry is witnessing significant advancements with the introduction of the newest mobile pump truck designs from leading manufacturers. These innovative units combine pumping power with unprecedented mobility, offering practical solutions for construction, mining, and emergency dewatering applications. The newest mobile pump truck models feature improved engine efficiency, smarter control systems, and enhanced durability to meet the growing demands of field operations.
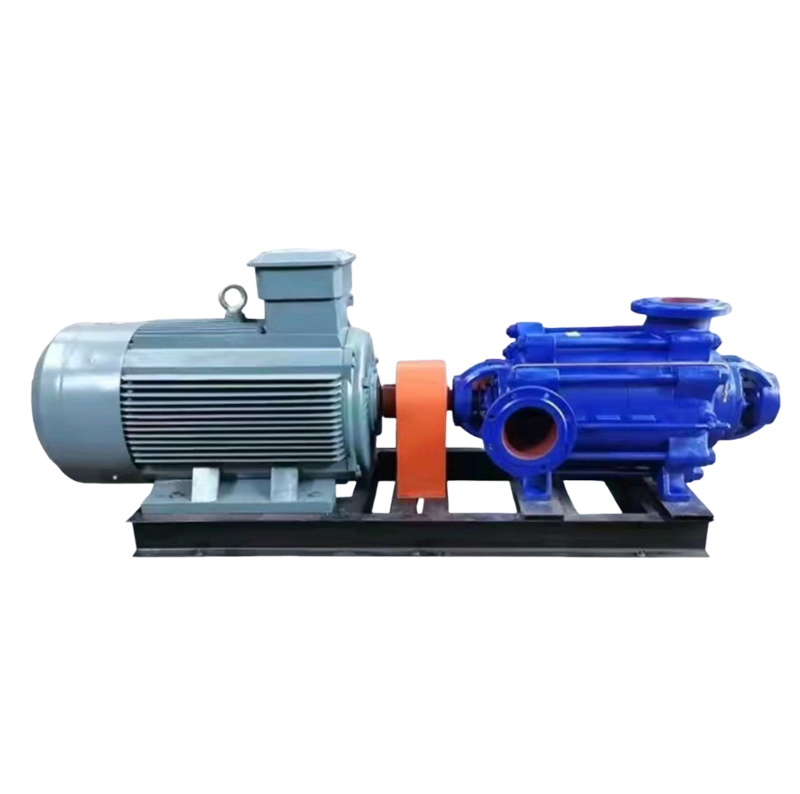
Understanding Double Suction Pumps: A Key Component in Industrial Applications
Double suction pumps are a critical component in various industrial applications, known for their efficiency in handling large volumes of fluids. These pumps utilize a unique design that allows water or other liquids to enter the pump from both sides of the impeller, effectively doubling the suction inlet area. This innovative engineering leads to several advantages, making double suction pumps a
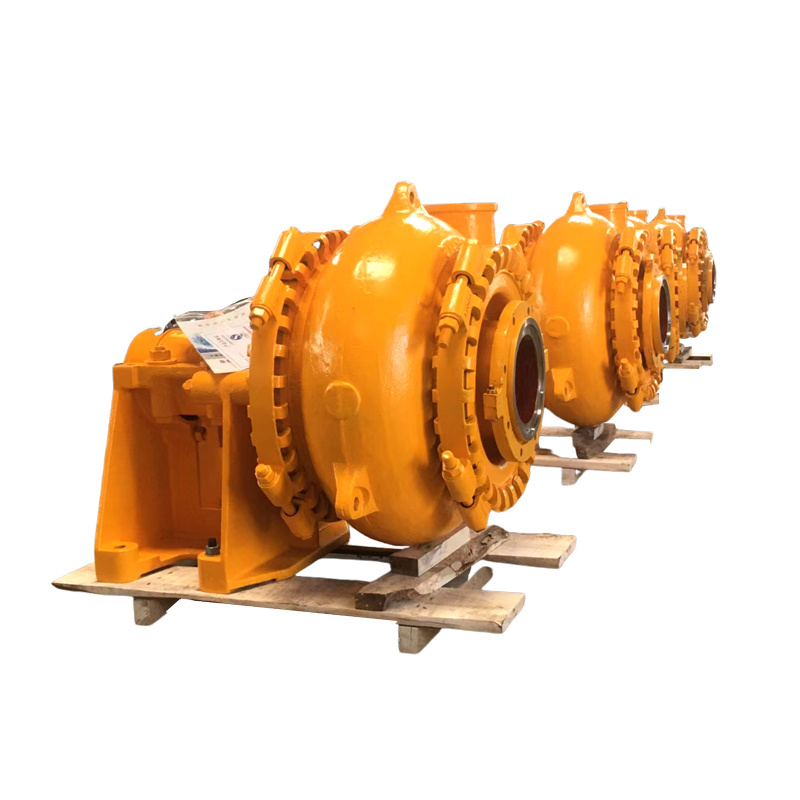
Durable Gravel Pumps from China Serve Mining and Dredging Needs
Wholesale gravel pump units manufactured in China are becoming essential equipment for handling abrasive materials in mining and dredging operations. These robust pumps specialize in moving slurry mixtures containing sand, gravel, and other solid particles, offering reliable performance where standard pumps would quickly fail. Their heavy-duty construction and specialized designs address the unique challenges of abrasive material transfer.
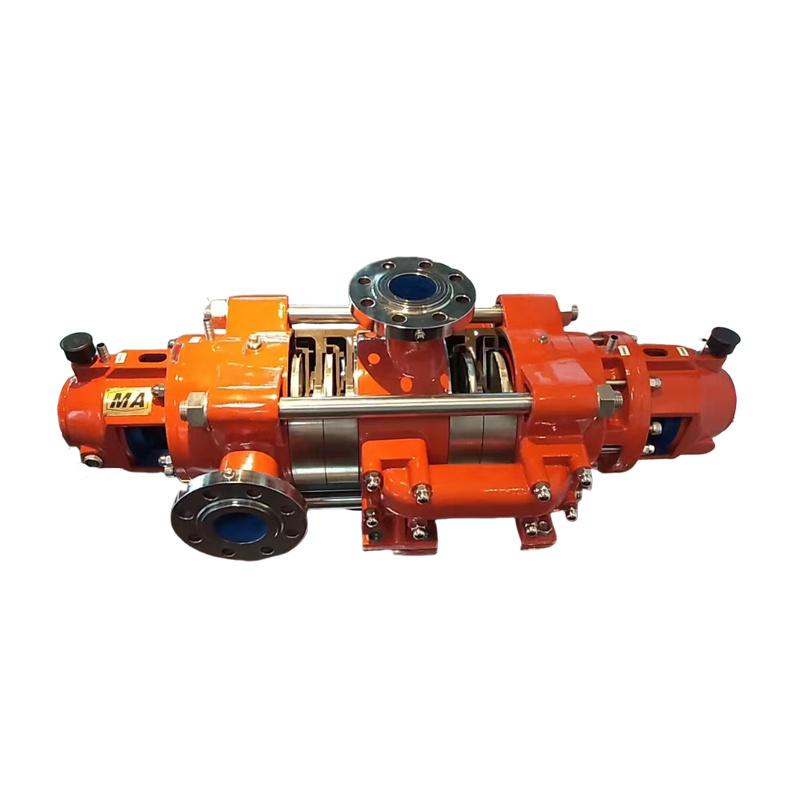
Understanding Multistage Pumps: The Versatile Solution for Various Industrial Applications
Multistage pumps are designed to handle a variety of applications in industrial settings. These pumps consist of multiple impellers, allowing them to generate high pressure and deliver significant flow rates. Their ability to provide increased pressure output makes them suitable for various industries, including water treatment, chemical processing, and oil and gas.
One of the key advantages of mu


Leave Your Message